Why our quality standards can protect your business
We conduct rigorous testing that directly translates into fewer customer complaints, warranty, and claim cases, which gives you a stronger brand reputation.
Products tested
Ensure that zero defective products reach your customers and protect your reputation.
Defect rate
Minimal warranty, claim, and service issues for you.
QA specialists
An average of 10+ years of experience to ensure consistent quality.
Years of experience
Proven quality systems you can trust and rely on.
What this means for your business success:
Reduced customer complaints
99.81% pass rate means almost no quality-related returns or negative reviews
Lower warranty costs
Rigorous testing minimizes defects and reduces warranty costs
Improved brand reputation
Consistent quality builds customer trust and drives more repeat purchases
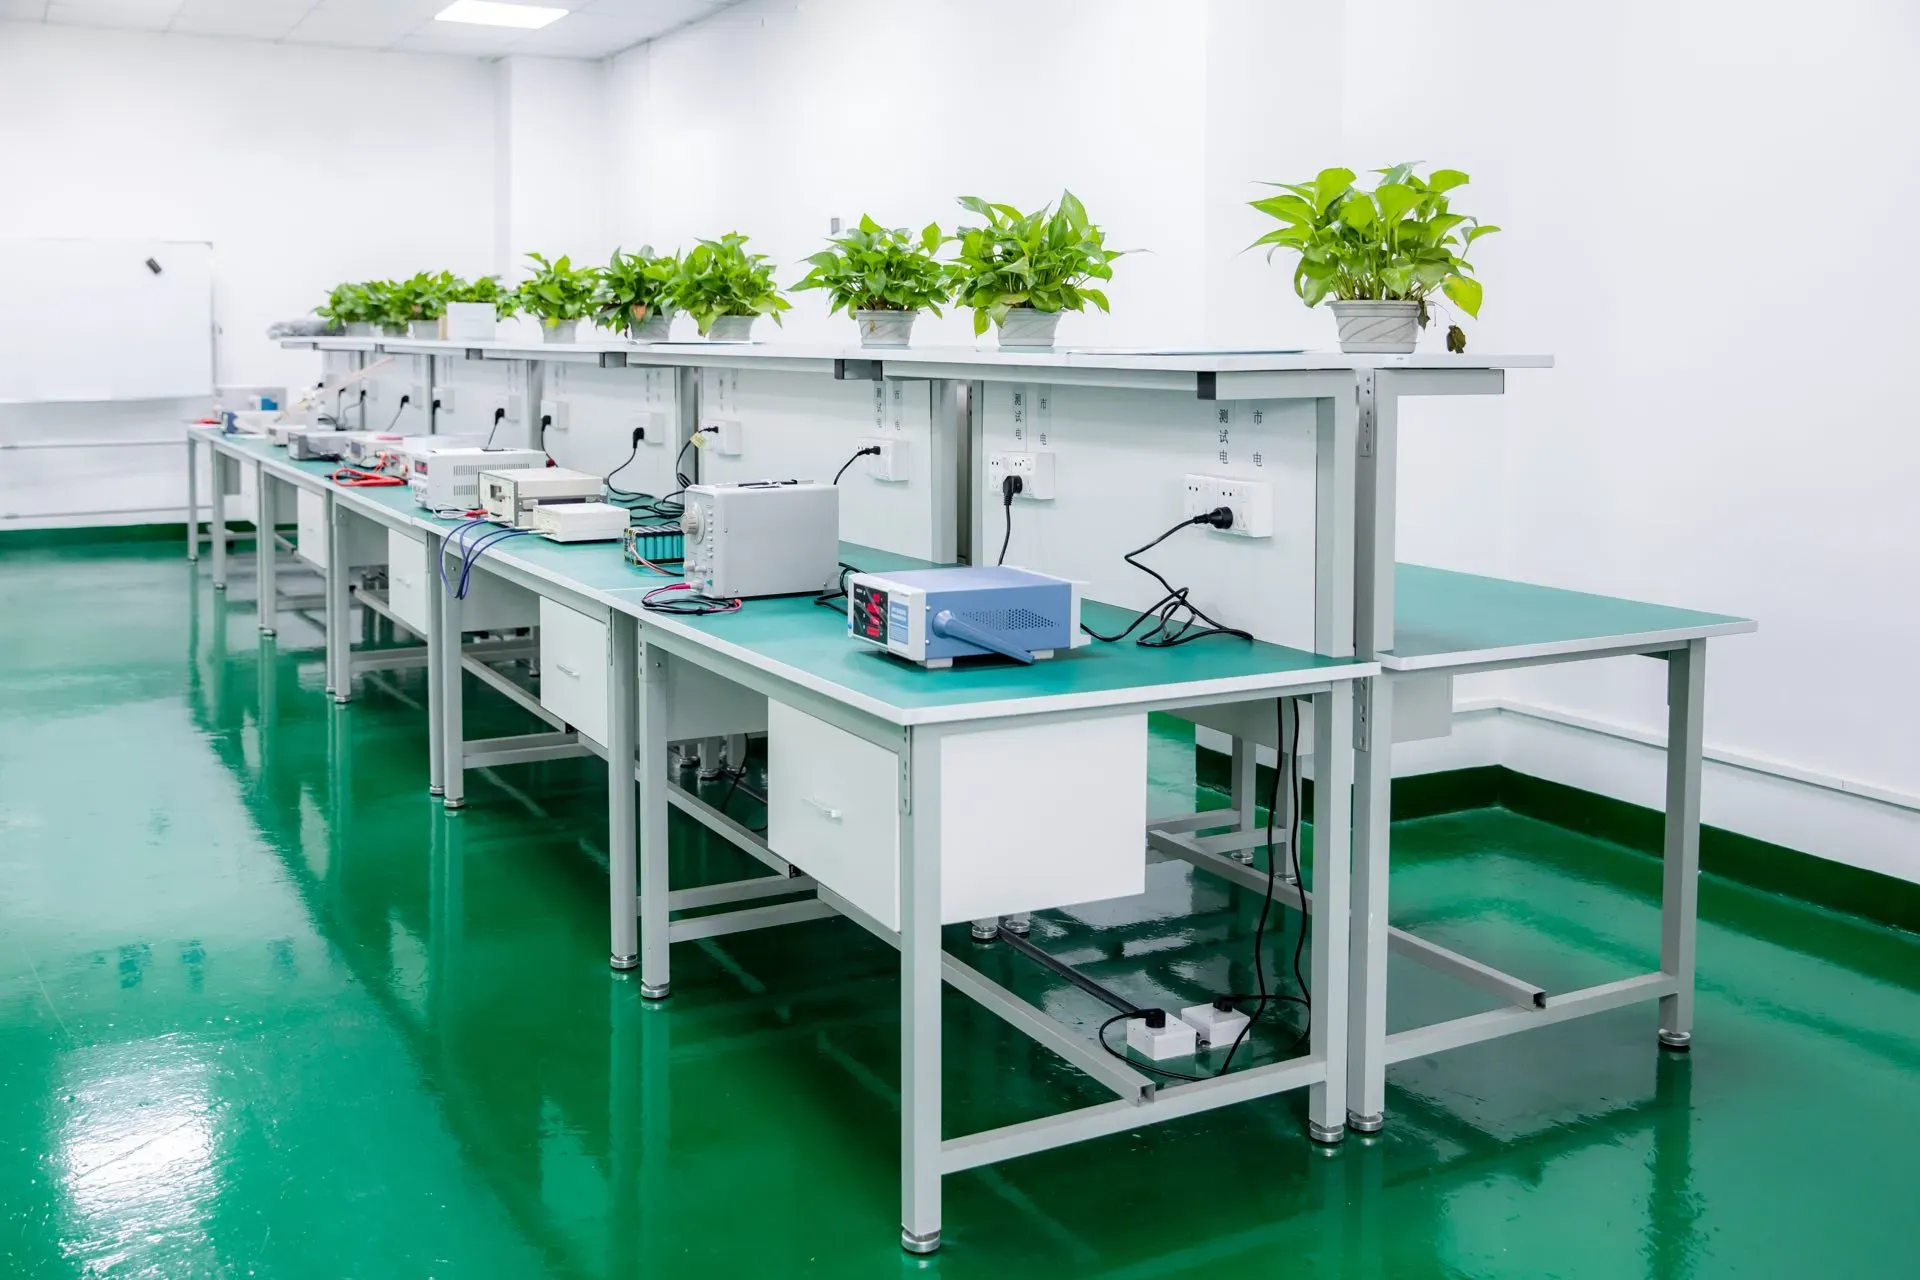
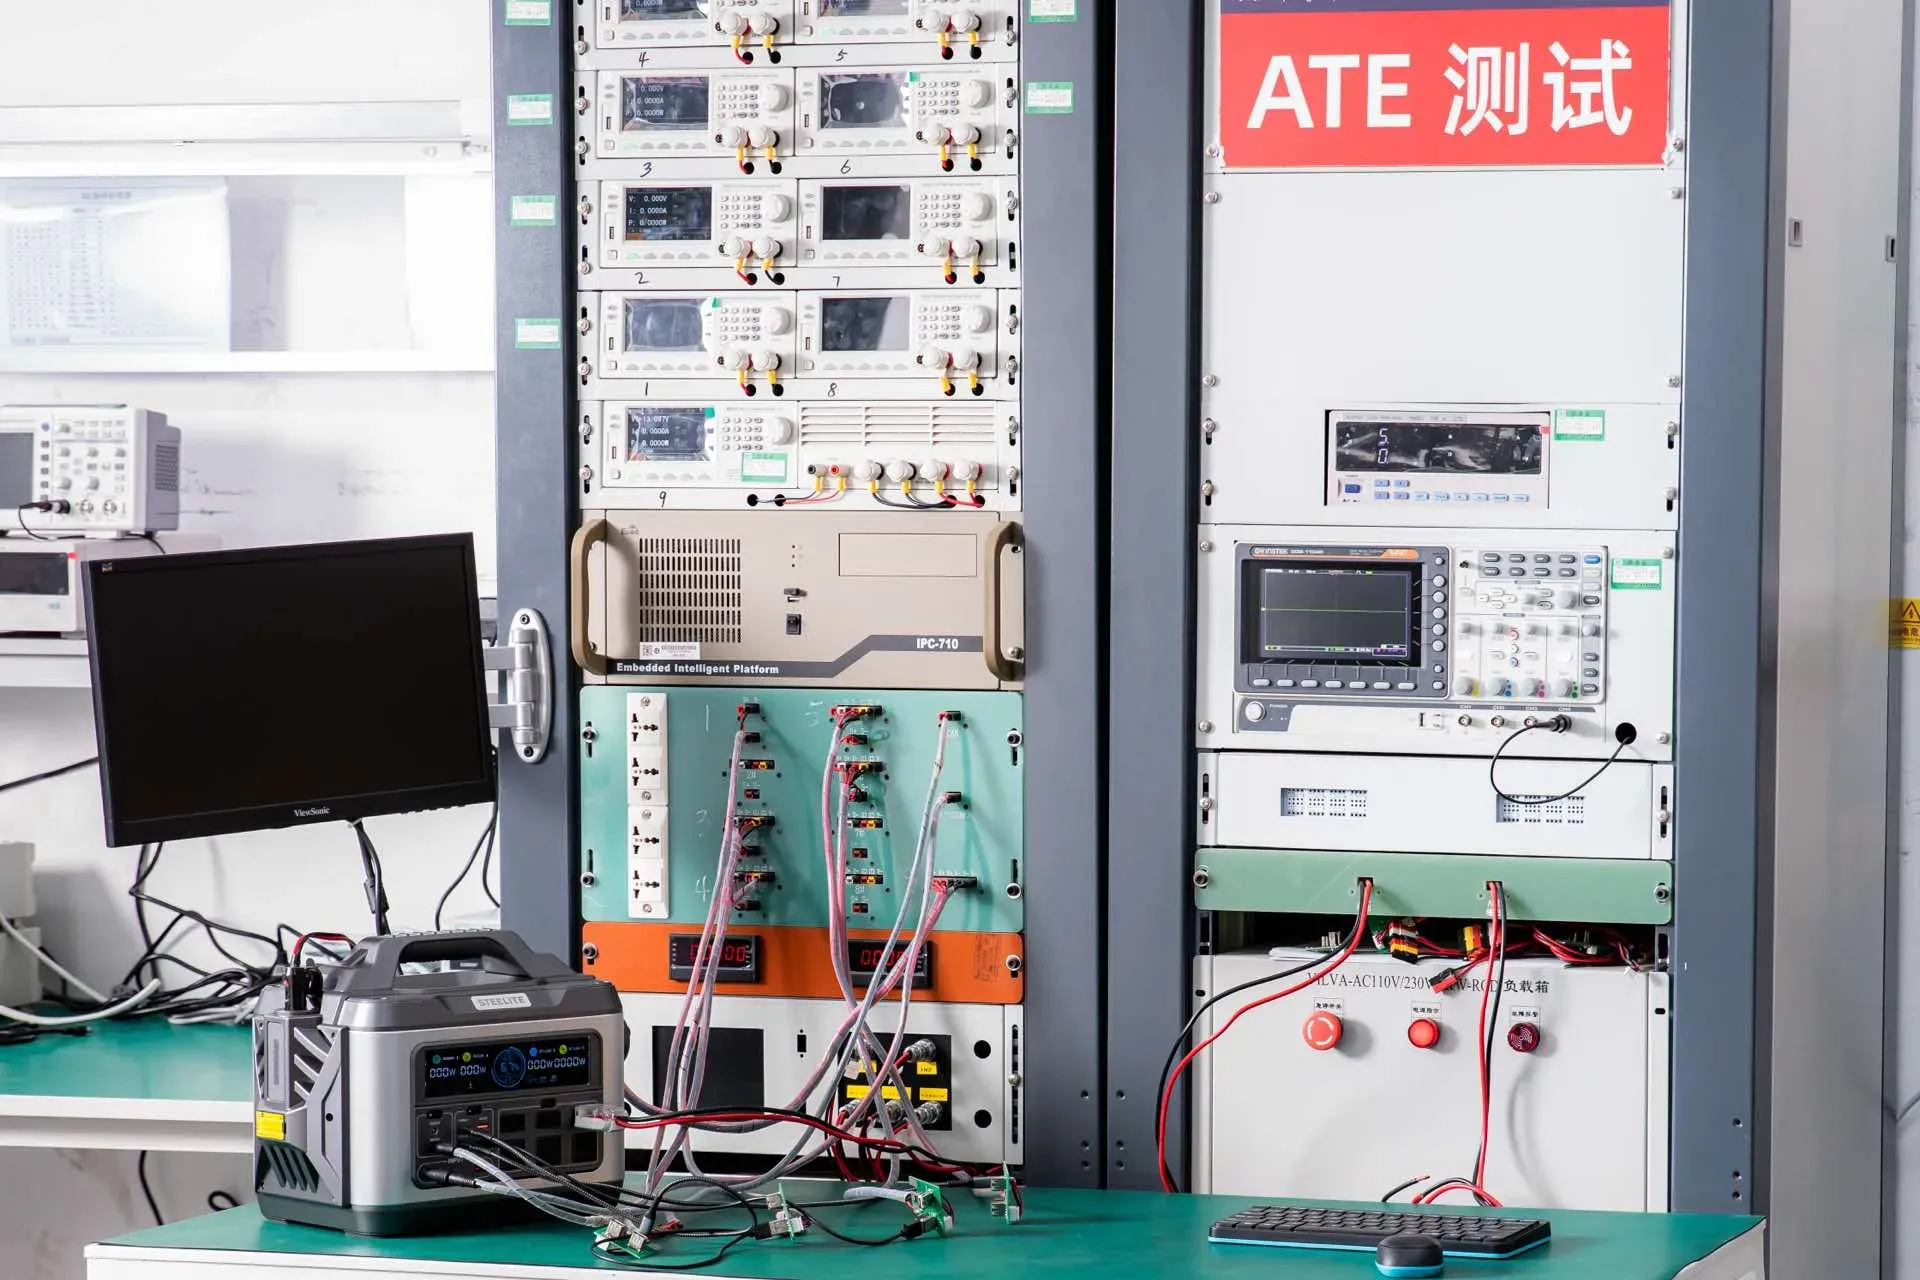
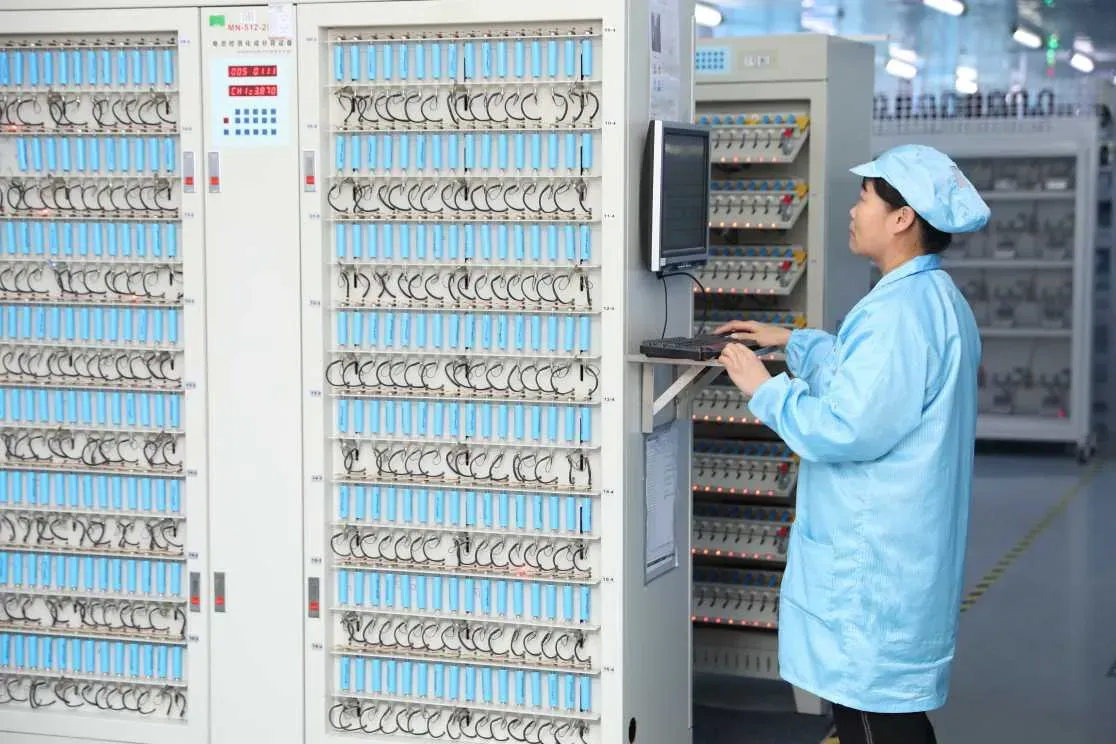
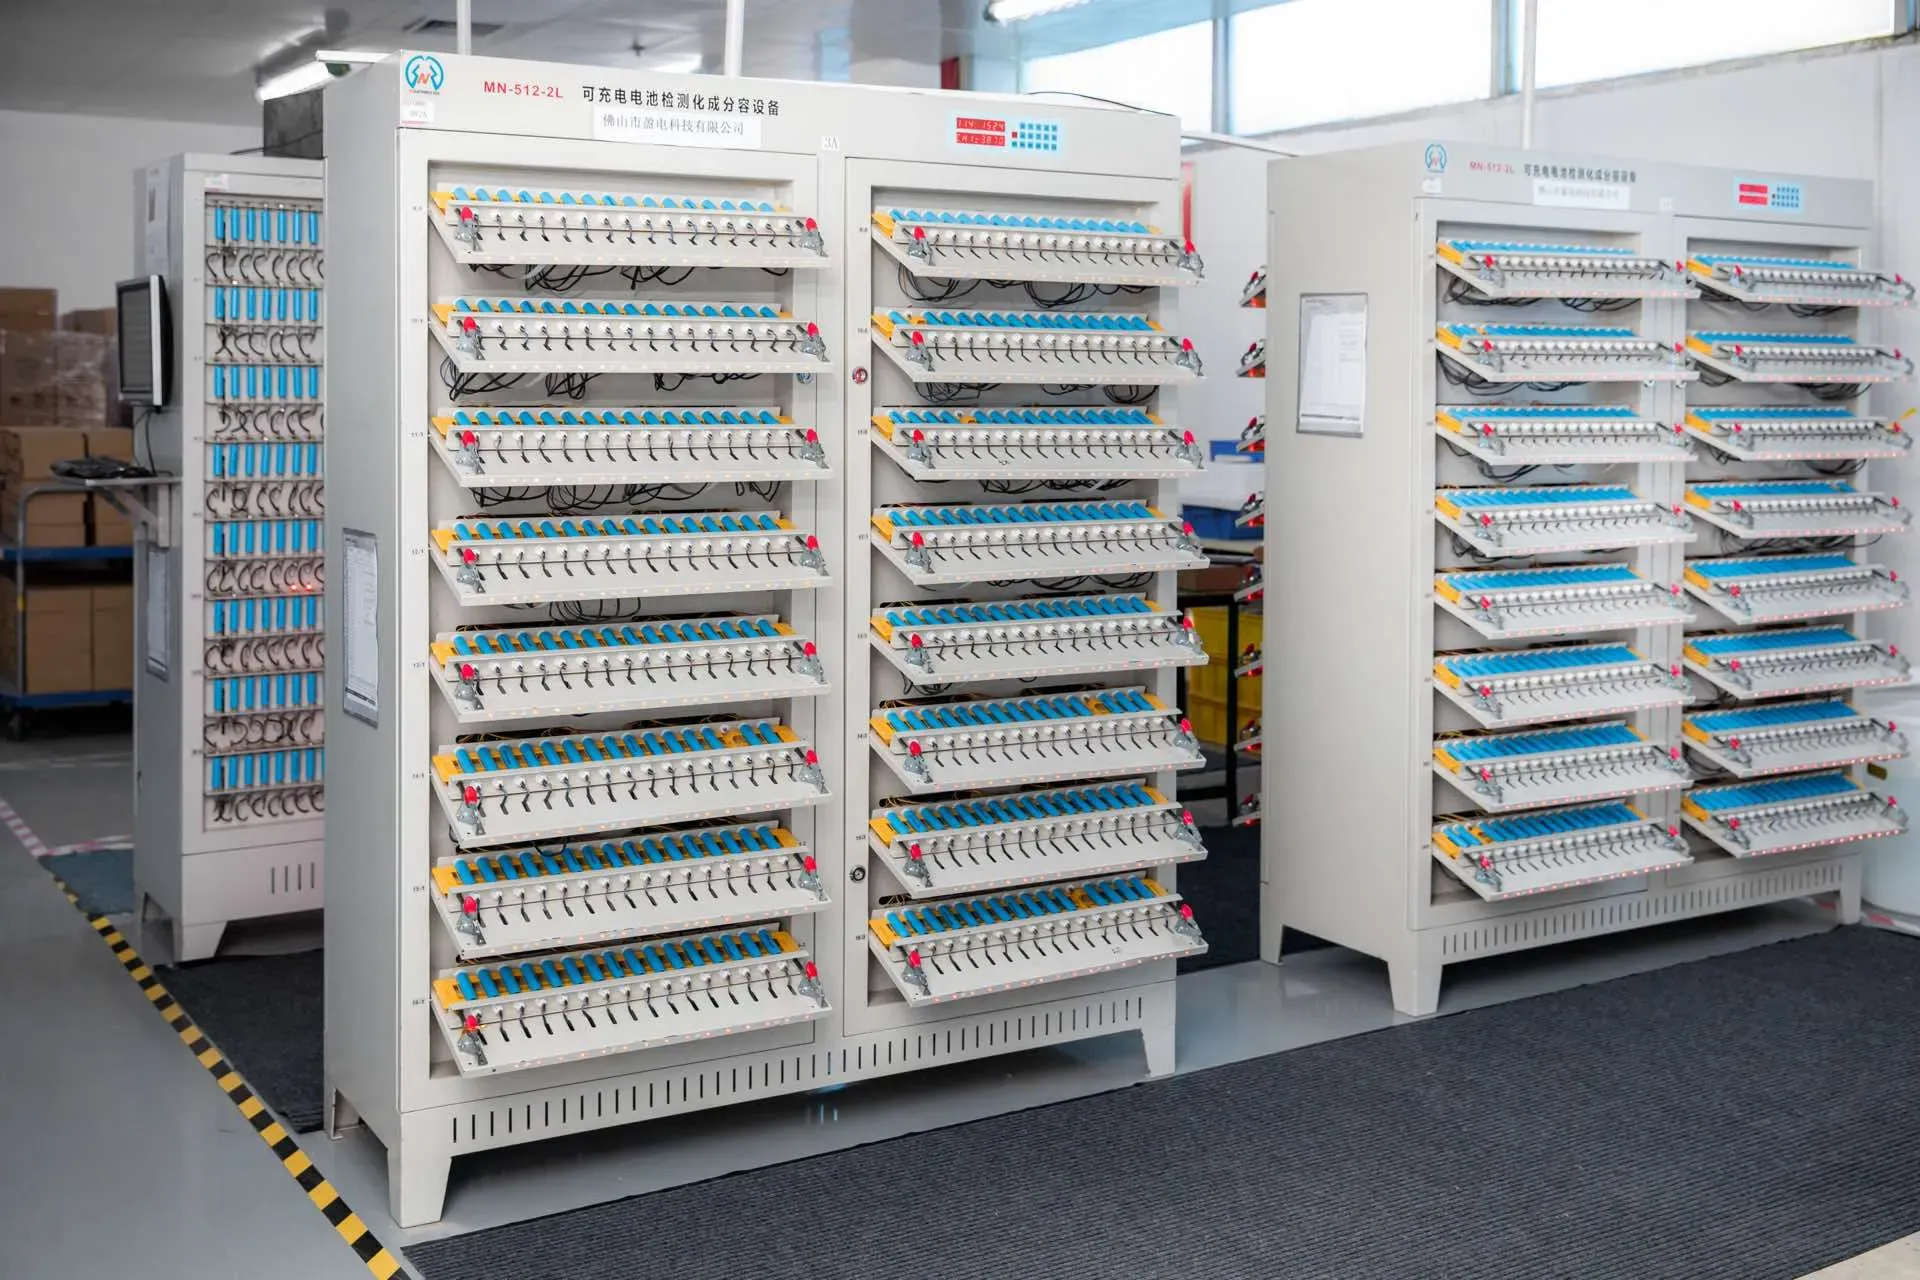
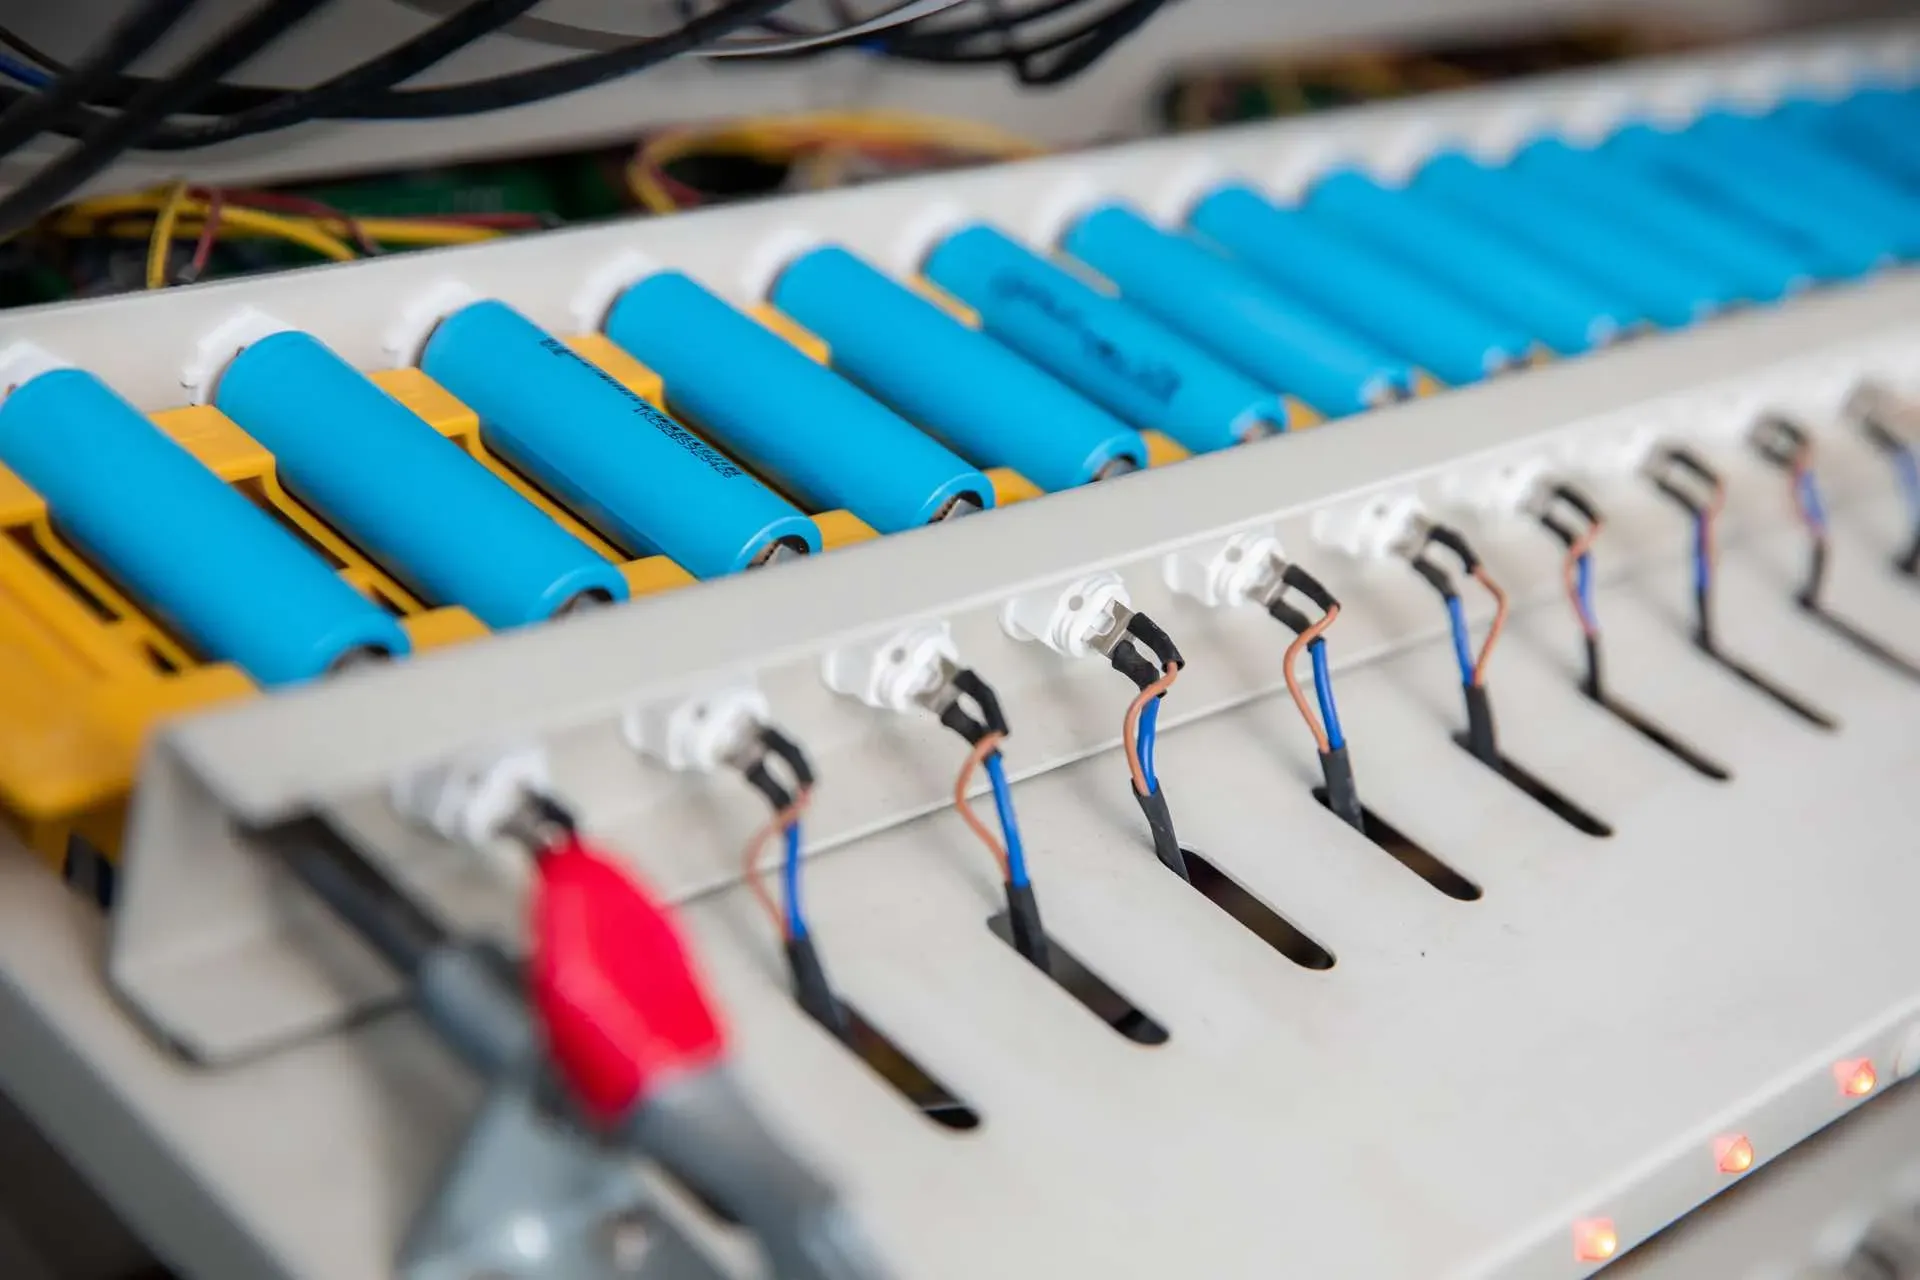
Our state-of-the-art quality laboratory
With the most modern testing equipment and strict protocols, we ensure that every product meets our high standards. Our laboratory is equipped with advanced testing devices that perform comprehensive tests at all stages of production.
Our 6-stage quality process protects your investment
Each stage is designed to eliminate specific risks and protect your business
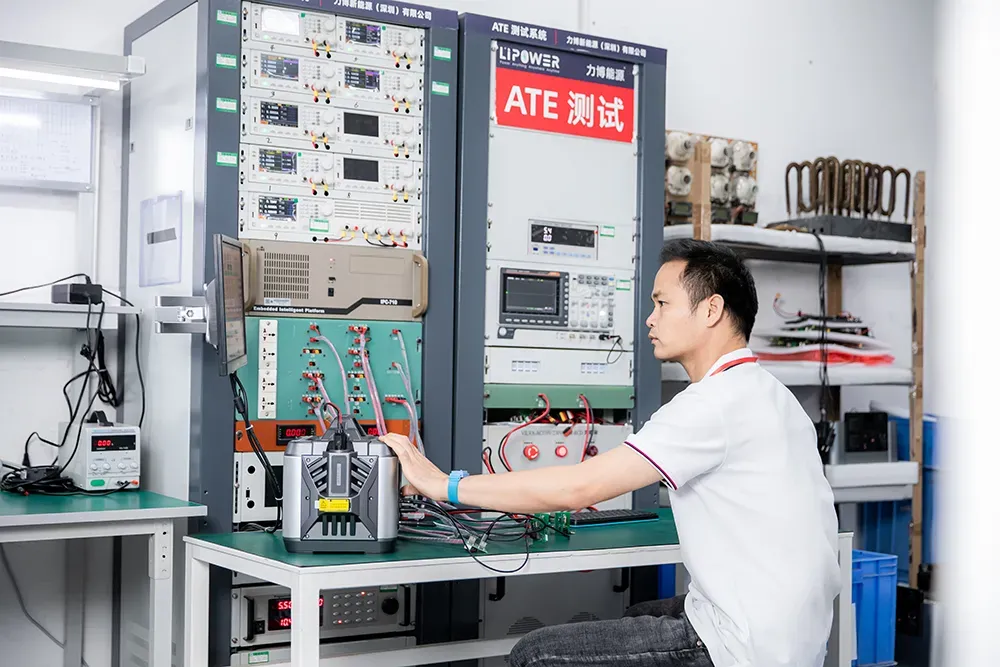
Basic functional verification
Each output port is tested with automated ATE machines to ensure your customers never receive a non-functioning product. This immediately eliminates returns and increases customer satisfaction.
Business impact:
- ✓ Zero „received defective" complaints
- ✓ Immediate customer trust
- ✓ Reduced customer service calls
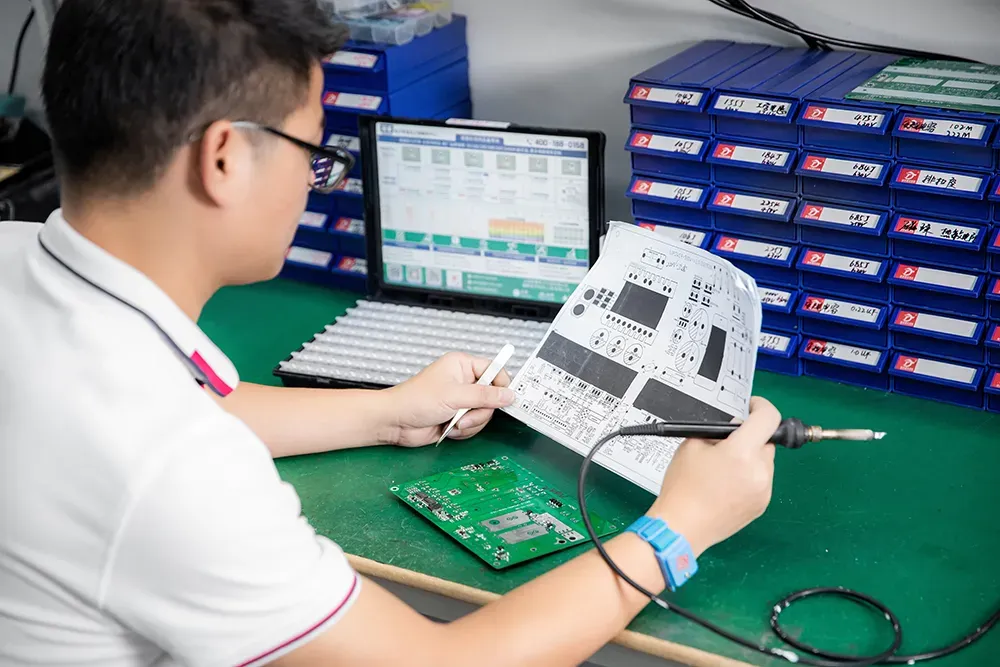
Circuit protection safety test
Advanced safety tests simulate circuit protection functions that should operate normally under overload, overcurrent, and short-circuit conditions. This protects your customers from safety risks and shields you from legal liability.
Business protection:
- ✓ Safeguards against security-related lawsuits
- ✓ Reduces insurance claims
- ✓ Meets international safety standards
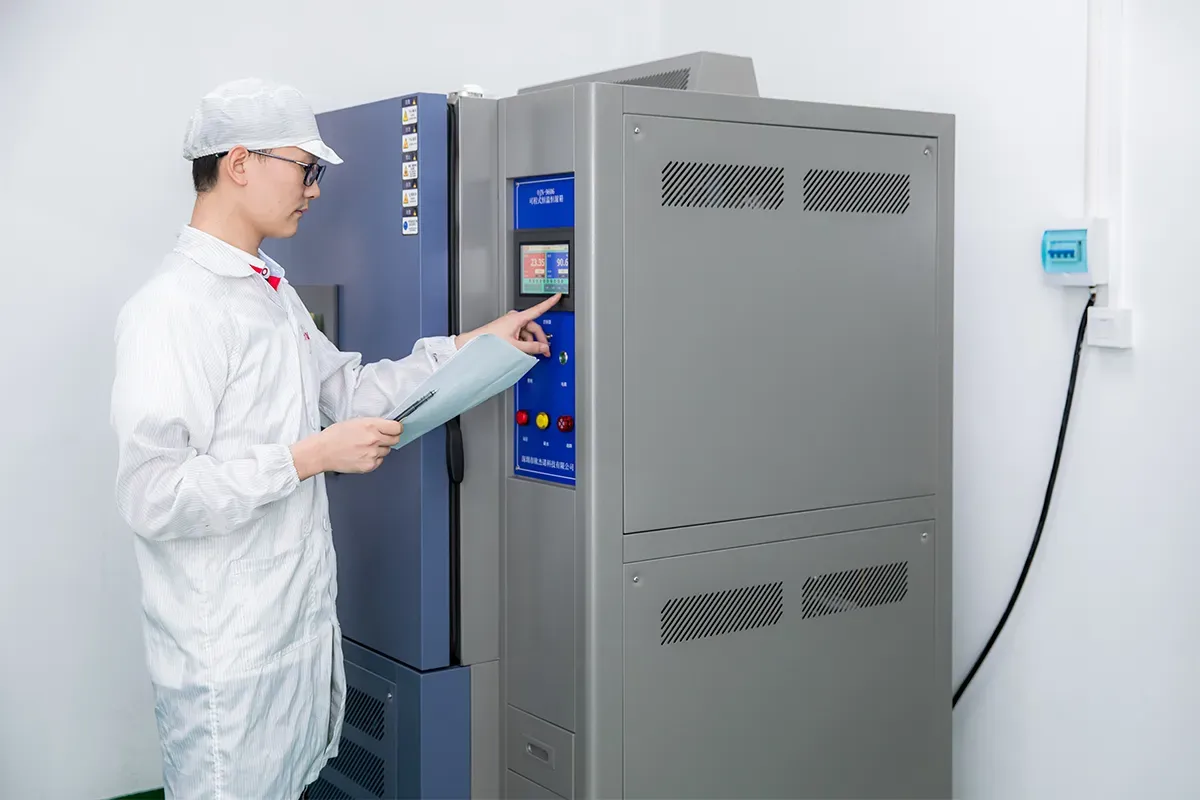
Extreme environment testing
The finished test product ensures it can operate normally from -30°C to 80°C.
Market advantages:
- ✓ Sell confidently in any climate
- ✓ Fewer temperature-related failures
- ✓ Expanded market opportunities
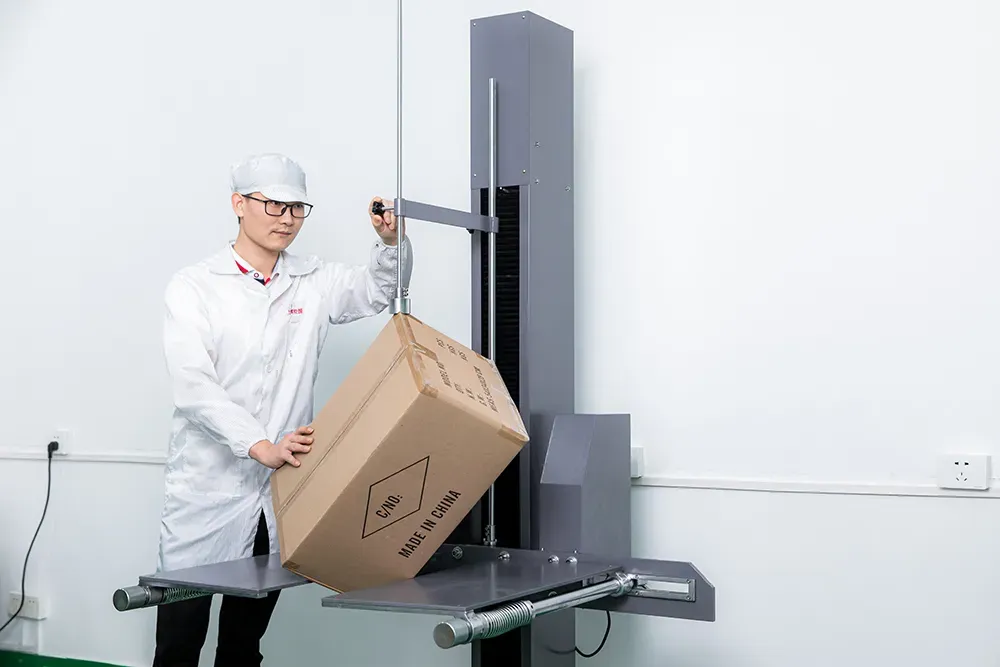
Durability and drop tests
Strict drop and vibration tests ensure the product continues to function despite risks during transport. This minimizes damage claims and shipping losses.
Logistics advantages:
- ✓ Reduced shipping damage claims
- ✓ Lower insurance costs
- ✓ Customer confidence in durability
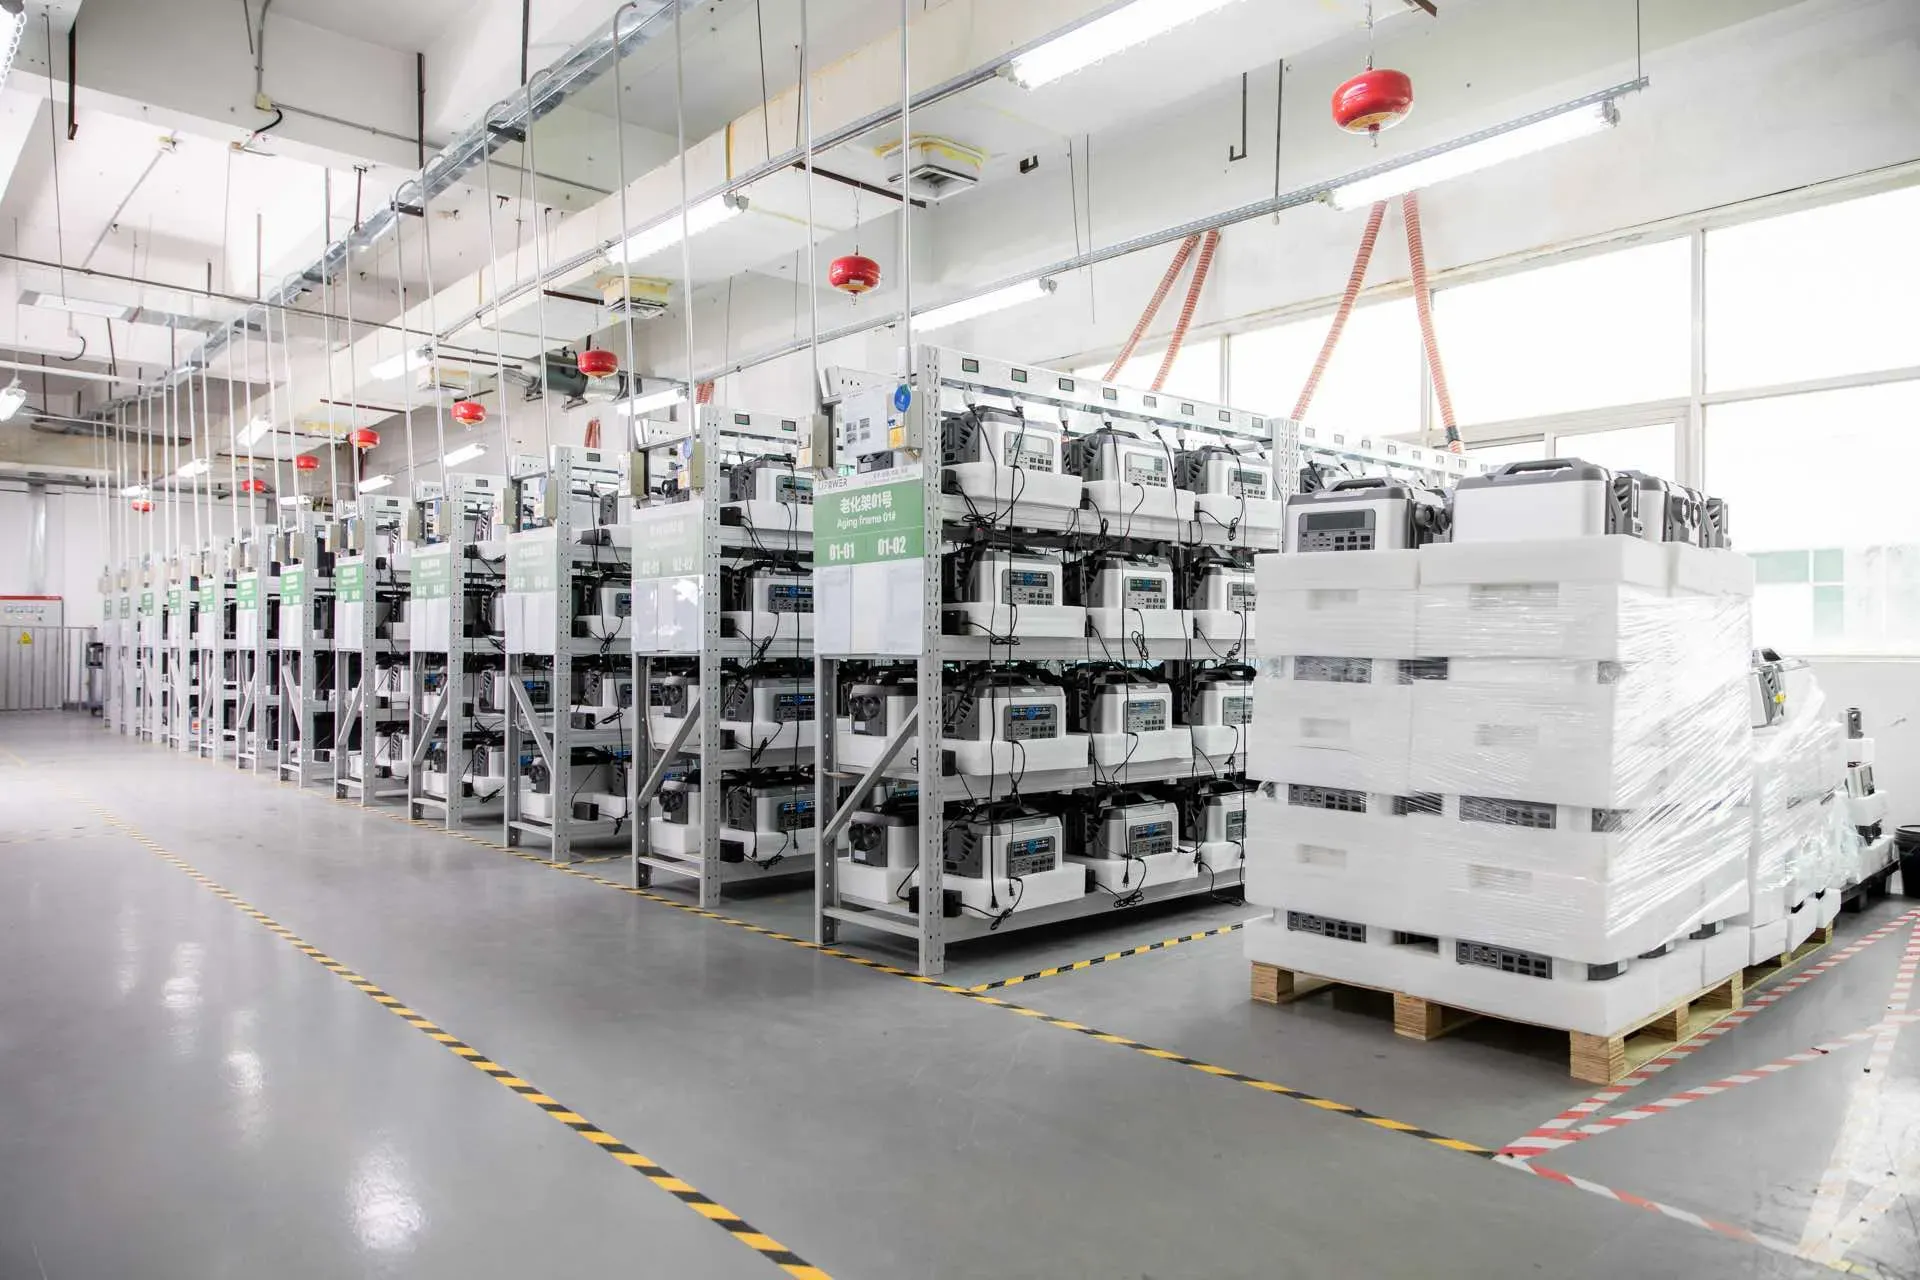
Comprehensive aging tests
All products undergo full charge-discharge cycles to identify early failures.
Long-term value:
- ✓ Prevents early field failures
- ✓ Extends product lifespan
- ✓ Creates customer loyalty
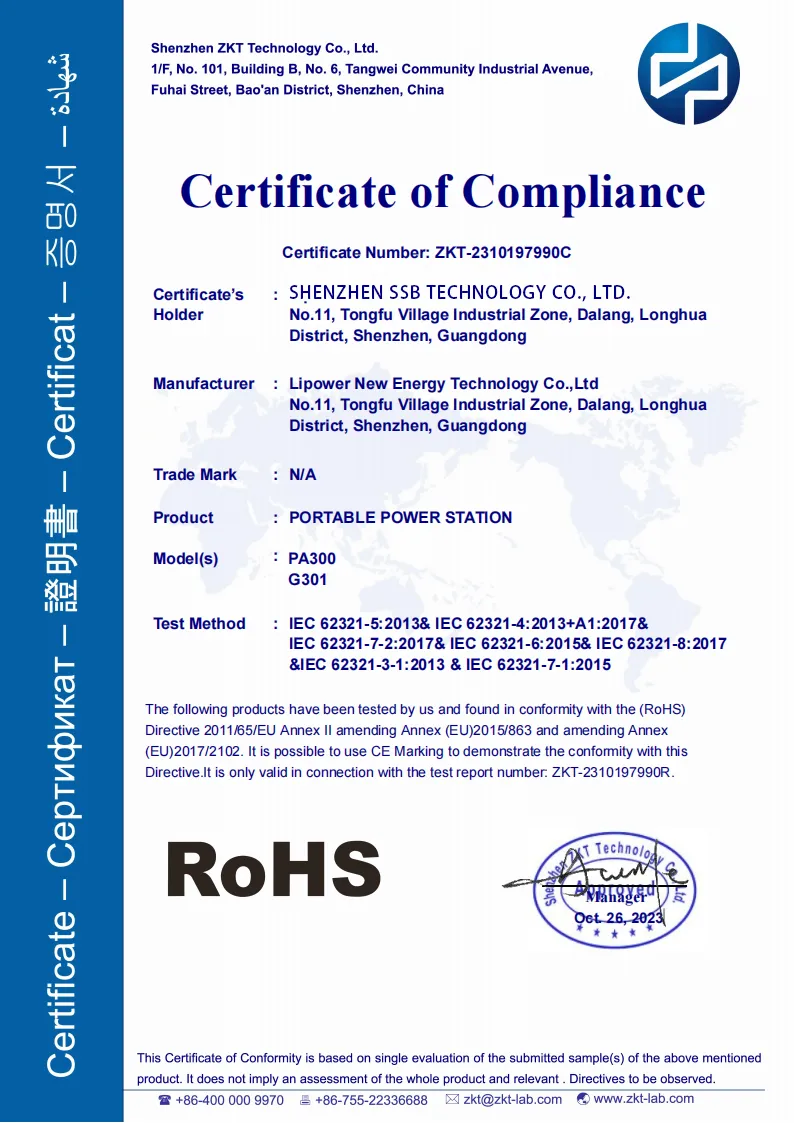
Final inspection and certification
Each product receives a final inspection and quality certification before shipment. This documentation protects the product during audits and gives your customers confidence.
Documentation value:
- ✓ Complete traceability records
- ✓ Audit-ready documentation
- ✓ Professional customer assurance
Our expert team
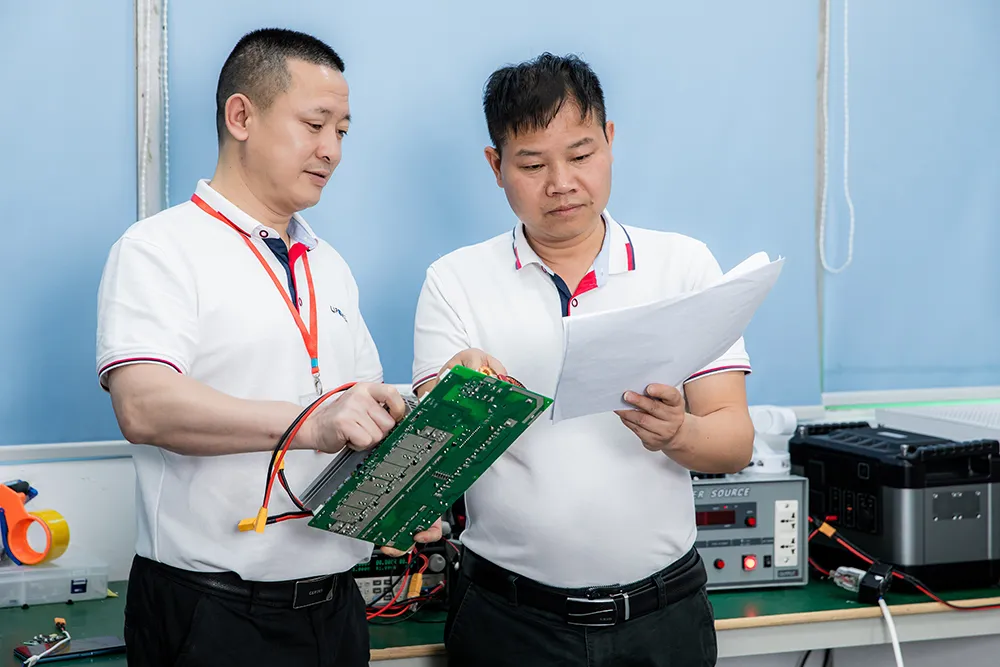
Our dedicated quality assurance team consists of highly qualified professionals with an average of over 10 years of experience in quality control and testing. They are the backbone of our quality promise.
Highly qualified specialists
Certified QA engineers with industry certifications
Continuous training
Regular updates on the latest testing standards and methods
Detail-oriented approach
Meticulous inspection of every single product
Data-driven decisions
Using advanced analytics for continuous improvement
Calculate your ROI
Our quality control not only prevents problems but also creates measurable business value for your company.
Quality Assurance Value Calculator
(98% improvement)
Without quality control
- ✗5-15% product return rates
- ✗High service costs
- ✗Reputational damage and loss of revenue
- ✗Increased warranty costs
- ✗Potential liability for safety
With LIPOWER quality systems:
- ✓0.21% TP3T error rate (99.81% TP3T pass rate)
- ✓Minimal customer complaints
- ✓Strong brand reputation
- ✓Reduced operating costs
- ✓Competitive advantage in the market
Would you like a personalized ROI analysis for your business?
Request free ROI consultationReady to protect your product quality?
Let us discuss how our quality systems can strengthen your business
 English
 German
 Spanish
 French
 Ukrainian
 Czech
 Swedish
 Belarusian
 Dutch